Admin@sciagglobal.com
Mon - Sat
10:30am - 7:30pm
Call us
+13099739581
We manufacture and supply premium-grade raw materials built to exact industry specifications — powering production operations worldwide with consistency, precision, and reliability.
Our production facility manufactures a wide range of agro-industrial raw materials that meet international quality standards and certification requirements.
Processed agro-based raw materials for fertilizer, feed, and food processing industries, produced under controlled conditions.
Specialty chemical raw materials for manufacturing, pharmaceutical, and processing industries with full traceability documentation.
Sustainably sourced and processed bio-materials used across cosmetics, health, and renewable energy sectors worldwide.
Raw material compounds for the construction and building materials sector, engineered for strength and compliance.
High-purity raw ingredients for nutraceutical and health supplement manufacturing, meeting GMP and FDA-grade standards.
Tailored raw material blends produced to client specifications — ideal for manufacturers with unique compound requirements.
A rigorous, end-to-end process that guarantees quality at every stage — from raw input sourcing to final product dispatch.
We procure base inputs from certified, vetted suppliers across global agro-industrial markets.
Every input batch is tested in our in-house laboratory before entering the production line.
Materials are processed using industry-standard equipment under controlled facility conditio
Finished products are certified against international standards before packaging and dispatch.
Products are packaged to export-grade standards and handed to our logistics network for delivery.
Built for scale, designed for precision. Our facility is equipped to handle high-volume orders without compromising on quality or turnaround time.
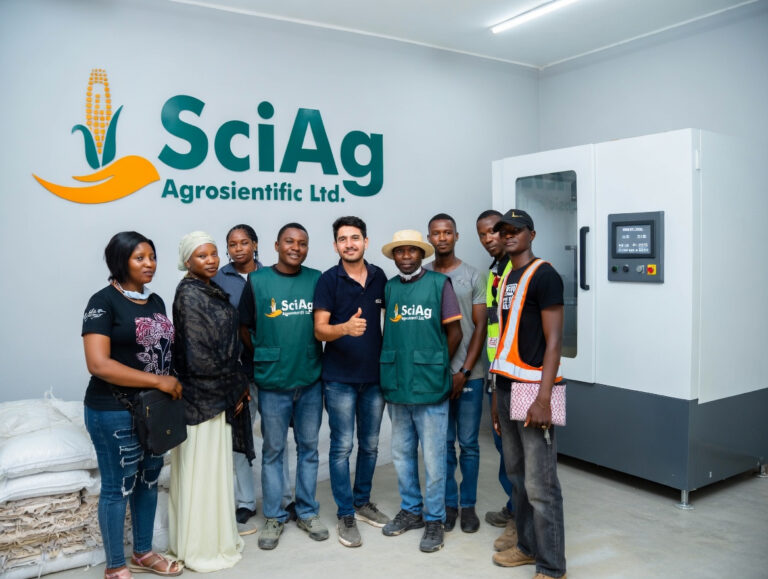
Our facility is designed for large-scale production runs, enabling consistent output to meet global demand.
All production lines operate under ISO-certified processes, ensuring international compliance at every stage.
A dedicated QA lab conducts rigorous testing on all inputs and outputs before they leave our facility.
We accommodate client-specific formulations and custom batch requirements with full documentation support.
Products are packaged to international export standards, ready for global distribution and customs clearance.
Every product that leaves our facility meets or exceeds global industry standards. Quality is not a checkpoint — it's built into every stage of our process.
Our processes are certified under ISO quality management standards for manufacturing excellence.
Independent laboratory testing is conducted on all product batches to verify quality and composition.
Every batch is fully traceable from raw input sourcing to final delivery with complete documentation.
Materials produced in compliance with international regulations for export to all target markets.
We are a leading scientific company dedicated to supplies quality lab equipment for Biotech, Medical, Educational and Government research.From Autoclaves & Balances to Viscometer baths and Water purifiers, SciAg will give you the best value prices. Our specialist staff can ensure your new equipment will include all the accessories for your test method, and can recommend the best solution, even if you don’t know exactly what you need.
© Sciag 2026. Designed By CeeHive